Seamless Tubing in Brass Musical Instruments
Like most industries, brass musical instruments benefitted greatly by the advances in technologies of the industrial revolution. The early industrial revolution (1760 to 1840) saw the invention and constant improvement of chromatic brass instruments that happened in this era. The trombone existed before this era, but also saw improvements, both acoustical and mechanical. This was made possible by materials, tools and processes developed during this acceleration of human understanding of the world they inhabited and how to exploit it. While musical instrument makers capitalized on the advances made in other industries as best they could, it would never be a sector that would lead in those advances. Production of textiles, iron and steel, machine tools, agriculture and advances in communication and transportation, being universally desired and demanded, would be the leading industries, but development of markets with smaller demands benefitted and progressed.
This introduction is background for the question that this article attempts to answer or at least shed light on with informed speculation. The puzzling question is: Why was the musical instrument industry so late in adopting seamless tubing? The easy answer is that tubing with seams worked just fine and it wasn’t worth any additional effort or cost. But why would it cost more or be difficult to obtain? Seamless brass and copper tubing was first developed on an industrial scale and patented in 1838 by Charles Green in Birmingham, England. This was a great improvement in boilers for steam engines that had previously relied on iron or brass tubing with soldered or brazed seams the length of each tube. Seamless brass tubes were superior, tolerating higher pressures and needing replacement at longer intervals. The demand was strong and by the mid-1860s, 85% of all steam engines in England were powered by boilers with seamless brass tubing and quickly spread to all of Europe and the United States. American Tube Works was in full production of seamless brass tubing for steam boilers in Boston by 1851 and were also widely promoting the superiority and lower cost for supplying water in residential and commercial plumbing in the 1860s.


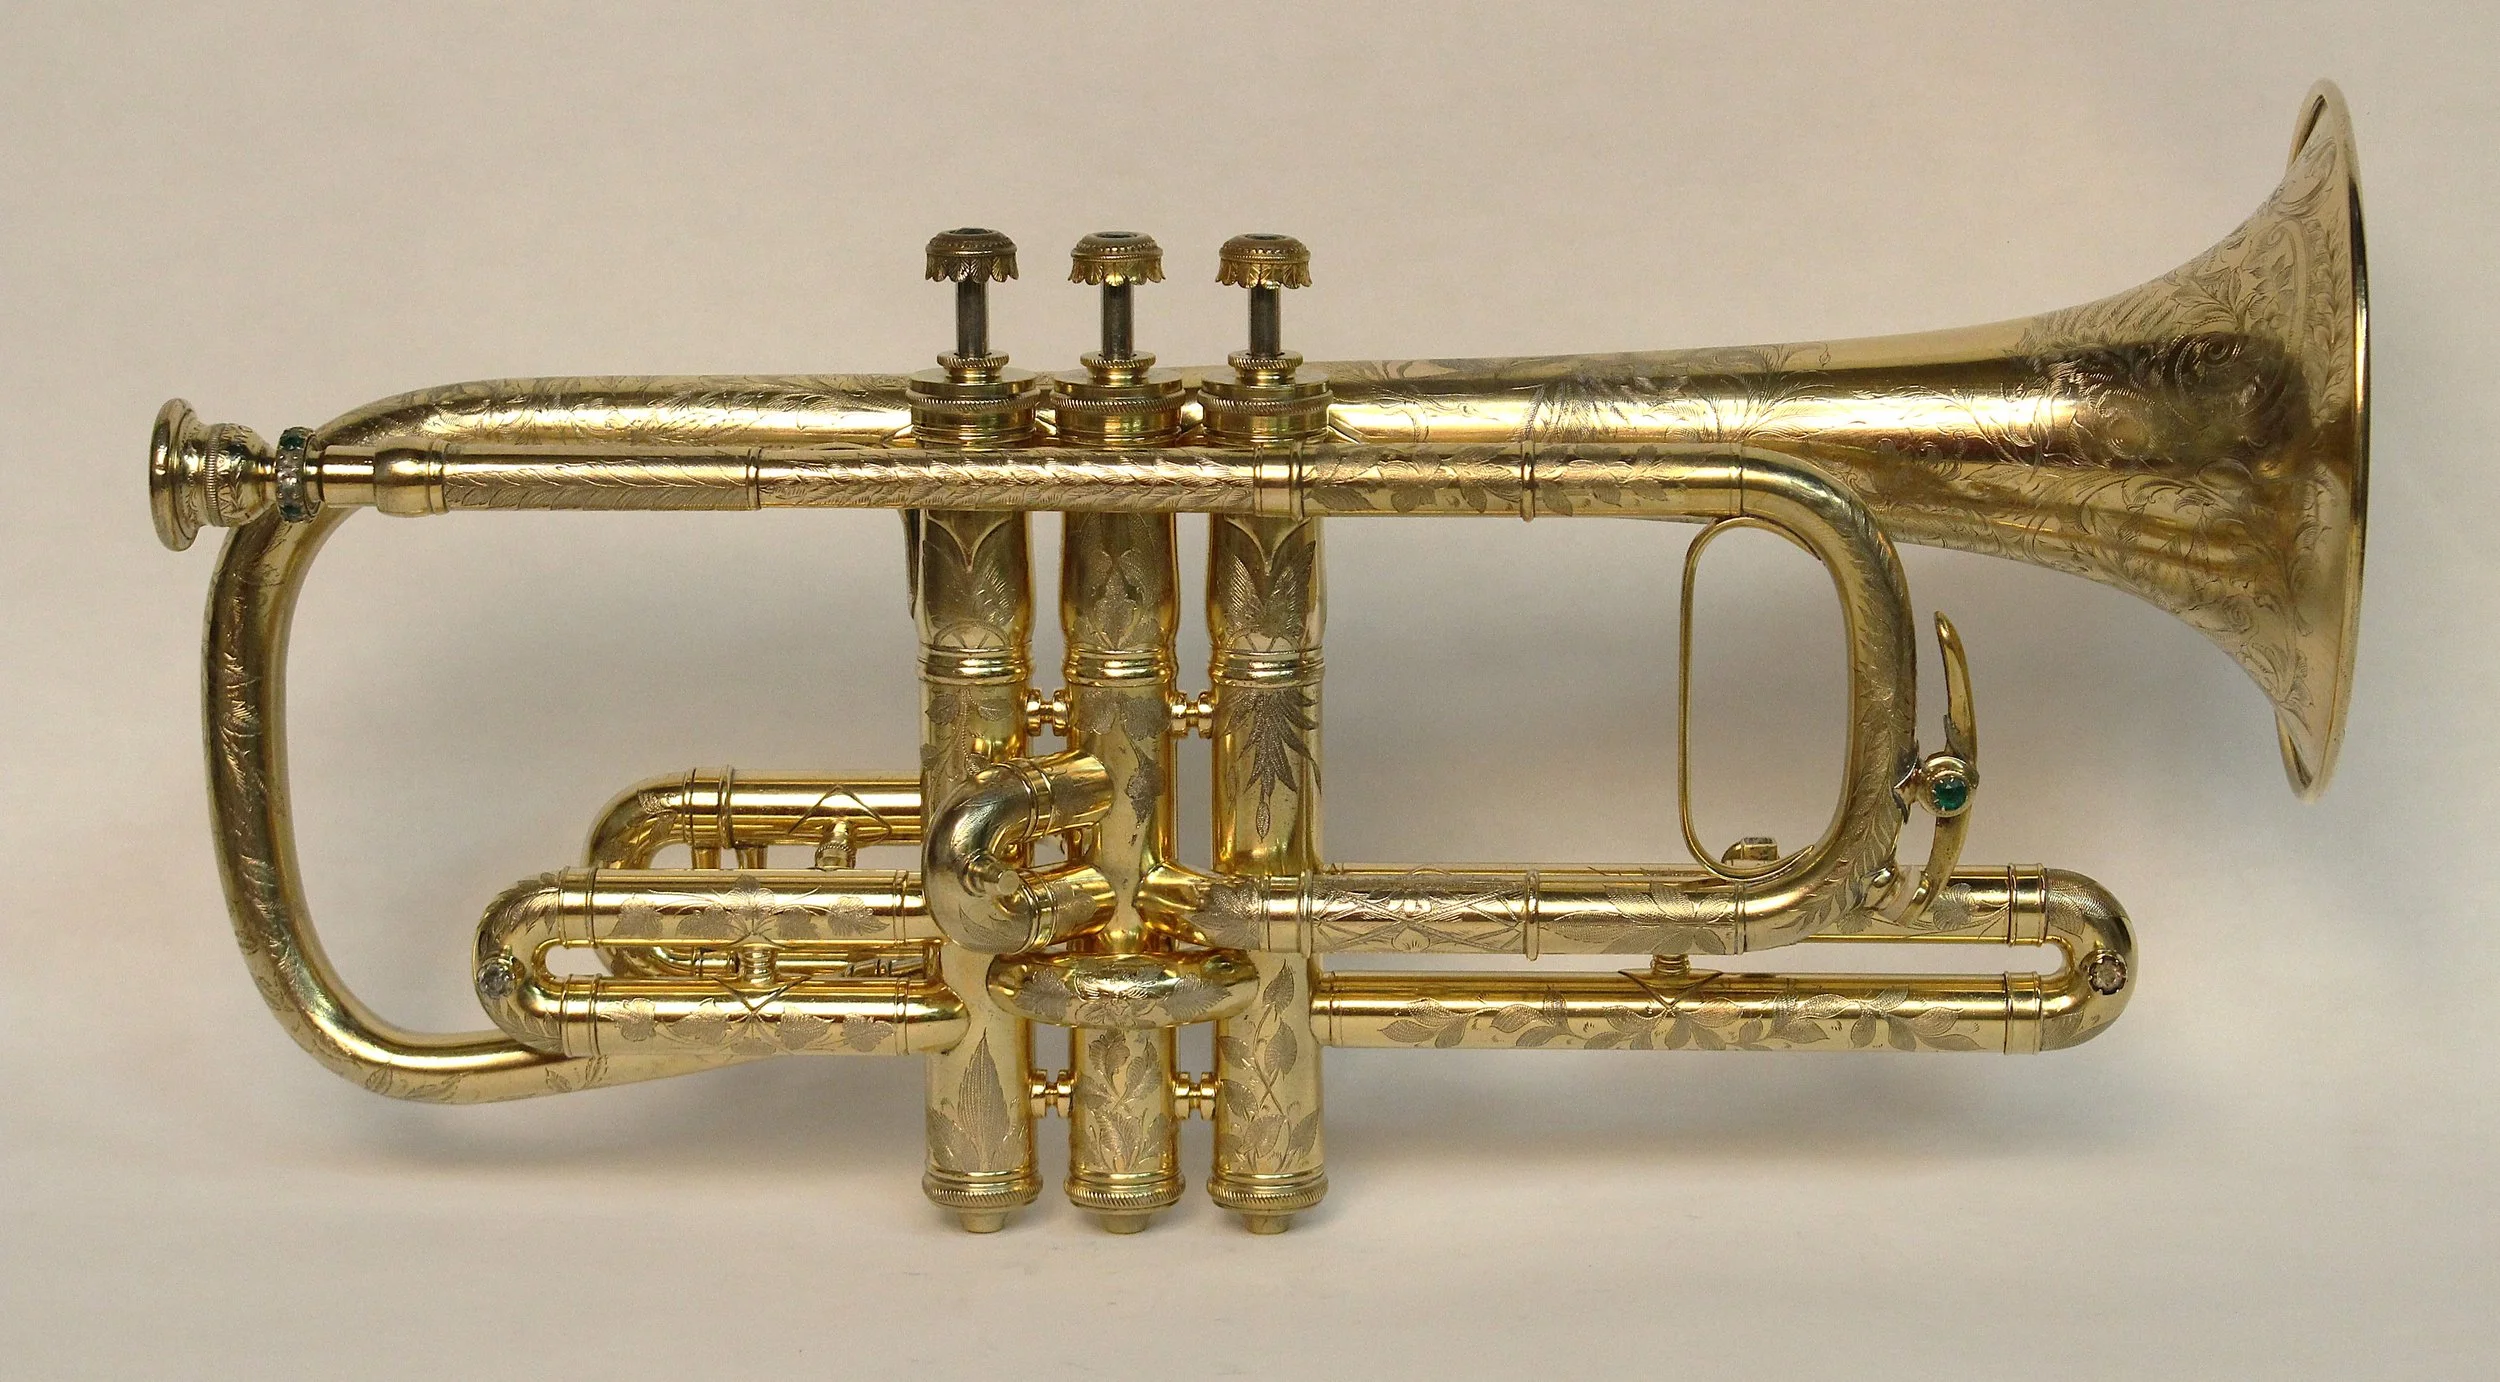
The earliest that seamless tubing is observed in musical instruments is in brass ferrules that reinforce the ends of wooden fifes. The year of manufacture can’t be determined on most of these, but the seamless ferrules are seen on fifes by Firth, Pond & Co. of New York made before 1863. In contrast, it was not seen in brass instrument tuning slide tubes until about 1900. The earliest seems to be C.G Conn in Elkhart, Indiana, although a larger scale survey will likely change these statements. Other US makers followed Conn’s lead very quickly, indicating that the economics of the supply chain were changing. Tubing for larger size instruments continued to be seamed for a short time longer and it is not unusual to observe seamless tubes in the valve slides, but seamed in the larger tuning slides. This might have been caused by what tubing was available, or the maker using up older stock more slowly on instruments sold in smaller numbers.
Smaller European makers were the last to incorporate tubing with seams in their production. The author has not found sources indicating whether this was a choice of individual makers or just what was available. In Germany, it became more common for makers to purchase standardized metric size tubing from large shops that specialized in that production, while American makers continued to purchase tubing in industrial standard sizes and then re-draw them to sizes that they required. Besson, in Paris, producing the trumpets that were considered the best and most copied, continued using tubing with seams until production was halted by war in the late 1930s.
It is possible that fife makers were able to obtain short pieces of seamless tubing that were trimmed from longer tubes as they were installed in boilers or utilize old boiler tubing when removed from service. When boilers were in constant service in both locomotive and stationary applications, the brass seamless tubing would need to be replaced about every three years. The more likely explanation is that these short brass tubes for ferrules were produced using the same method as brass firearm cartridges. This involved pressing and then drawing them from a disk cut from a sheet of brass, annealing before each step. In 1858, Alexander Parkes of Birmingham, England was granted a patent for using this technique for making longer seamless copper, brass and nickel silver tubing. It states that “the thickness of the original discs are to be proportioned to the length and thickness of the metal of the finished tubes”. It doesn’t clarify if this means that the center of the disk is thicker than the outer edges or just overall thickness. In the latter case, the tubes wall thickness would be far greater at the open end the closed end formed from the center of the disk and would require more force and additional annealing and drawing steps to result in uniform wall thickness. The patent does not specify the lengths of finished tubes, but they would have been long enough for making brass instrument tuning slides.

The seamless tubes needed for steam production were typically six to eight feet long. These were produced by first casting a short, thick-walled tube that was then drawn longer and thinner, annealed, and the process repeated, typically five times, until they were the dimensions needed. Flaws in the initial casting wouldn’t be found until they failed during one of the subsequent drawing steps, which added to the cost of this process and added incentive to improve alloying and casting technologies. Another innovation from this time was to make the final draw onto a mandrel with a slight taper, so that the tube’s wall thickness would be greater at one end. The thicker end was installed closest to the firebox, and would last longer before leaking and needing repairs and ultimate replacement.
By 1866, six factories in Birmingham, England were producing 6500 tons of seamless brass tubing each year. These same factories also produced brass tubing with seams, presumably at lower cost. Even small makers, such as Graves & Co. of Winchester, New Hampshire had draw benches to produce tubes in the sizes needed for their production, but sources have not been found stating whether musical instrument makers made tubing from sheet metal or purchased tubes produced by specialized shops. In the 20th century, musical instrument makers purchased seamless tubing in standardized sizes from industrial suppliers and then drew them to the sizes that they required. If the the maker was large enough they could afford to order mill runs (usually several thousand pounds) of a more specialized material such as nickel silver (German silver). In that case, they could specify the alloy and other requirements such as state of hardness. The latter could be a large savings, if delivered “dead soft” or fully annealed and ready to re-draw.
Most of the information in this article was taken from sources found by research by Steve Dillon.
As with most pages on this website, this is a subject of ongoing inquiry, to be updated as additional data is discovered. Your feedback is always welcome.
robb@robbstewart.com